
 English
 中文简体

Oxygen Barrier Packaging: How OTR Values and Material Choice Affect Shelf Life
 2026.09.21
 Industry News
Oxygen barrier packaging is not one material but a category of solutions built around a single question: how much oxygen can pass through a package over time? The answer determines whether a bag of coffee keeps its aroma for six months or two weeks, whether sliced meat stays red or turns brown, and whether a pharmaceutical blister pack protects its contents across an entire supply chain.
If you specify flexible packaging for food, beverage, or pharmaceutical applications, the practical starting point is straightforward: choose the material with the lowest oxygen transmission rate (OTR) that still fits your product, process, and budget. This guide explains how oxygen barrier packaging is measured, which film families deliver the strongest performance, and how to match those materials to real product requirements.
What Is Oxygen Barrier Packaging?
Oxygen barrier packaging refers to any packaging structure designed to prevent or significantly limit the passage of oxygen from the external environment into the package. The purpose is to slow oxidation reactions that degrade product quality, alter flavor and color, and ultimately shorten shelf life.
Oxygen is a reactive gas that can trigger several failure modes inside a package:
- Lipid oxidation that creates rancidity in nuts, snacks, and cooking oils
- Color degradation in fresh meat, processed meat, and certain vegetables
- Nutrient loss, especially vitamins A, C, and E
- Growth of aerobic spoilage microorganisms in ready-to-eat products
An oxygen barrier is achieved by including one or more layers with low oxygen permeability in the laminate structure. These layers can be metallized films, transparent oxide-coated films, PVDC-coated films, aluminum foil, or EVOH-based structures.
How Oxygen Barrier Performance Is Measured
Two metrics define the practical barrier performance of any packaging film. Both are measured under standardized conditions and are reported as a rate per unit area and time.
- Oxygen transmission rate (OTR): measured in cubic centimeters per square meter per day (cc/m²/day) at 23°C and 0% relative humidity, or alternatively at 50% RH.
- Moisture vapor transmission rate (WVTR): measured in grams per square meter per day (g/m²/day) at 38°C and 90% RH.
Lower values indicate better barrier performance. A standard PET film might have an OTR of 150-200 cc/m²/day. High barrier films are typically defined by OTR below 10 cc/m²/day, while ultra-high barrier structures can achieve OTR below 0.5 cc/m²/day.
High barrier threshold: OTR less than 10 cc/m²/day
Ultra-high barrier: OTR less than 0.5 cc/m²/day
| Film structure | OTR (cc/m²/day) | WVTR (g/m²/day) | Clarity |
|---|---|---|---|
| Standard PET | 150-200 | 20-30 | Clear |
| Metallized PET | 0.5-2 | 0.5-1 | Opaque |
| ALOx-coated PET | 0.5-3 | 1-5 | Clear |
| PVDC-coated BOPP | 5-20 | 3-10 | Clear |
| Aluminum foil laminate | <0.1 | <0.1 | Opaque |
The table shows that metallized films and oxide-coated films can approach aluminum foil performance while retaining the advantages of flexible films: lower weight, lower cost, and better flex-crack resistance.
Main Oxygen Barrier Material Families
Flexible packaging films that provide oxygen barrier performance can be grouped into three families. Each has distinct trade-offs between barrier level, appearance, and cost.
Metallized Films
Metallized films have a vacuum-deposited aluminum layer that delivers excellent oxygen and moisture barrier. The aluminum coating also provides a highly reflective, glossy appearance that improves shelf presence. For demanding oxygen barrier applications, two product lines are particularly relevant.
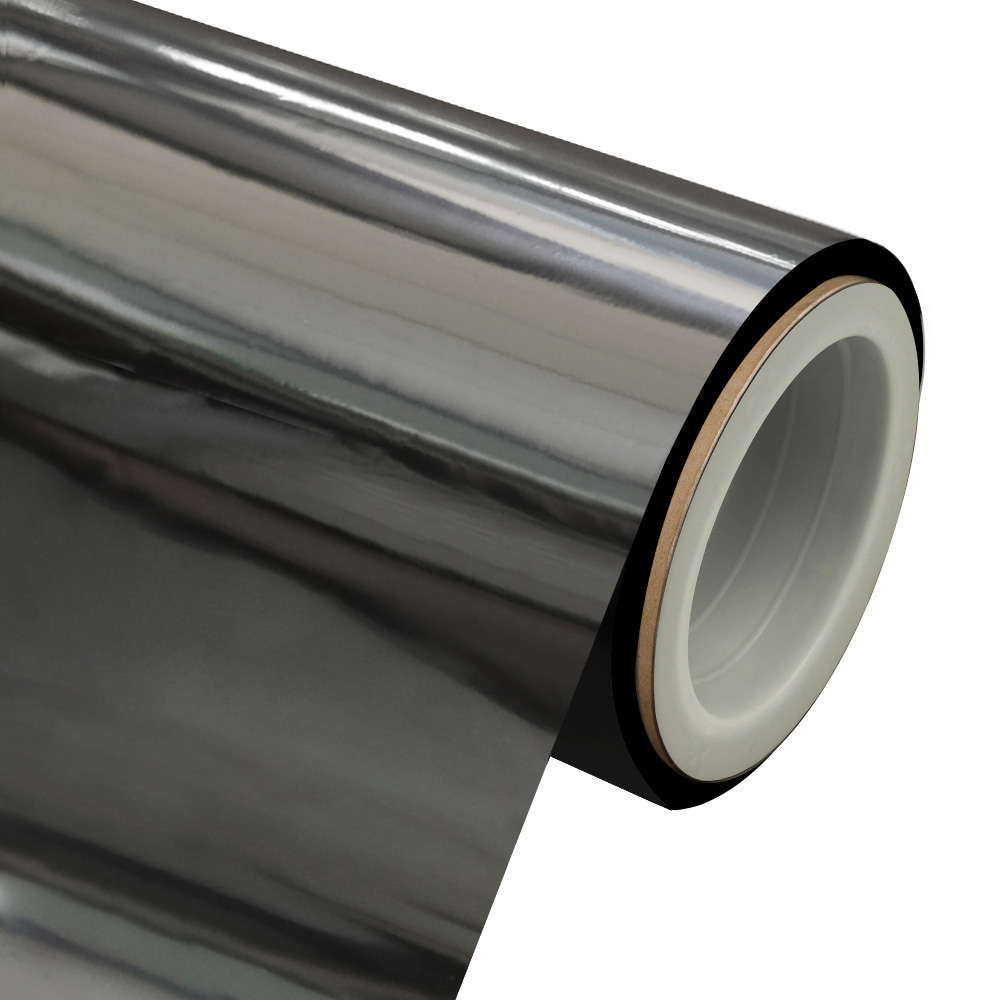
High-barrier metallized PET film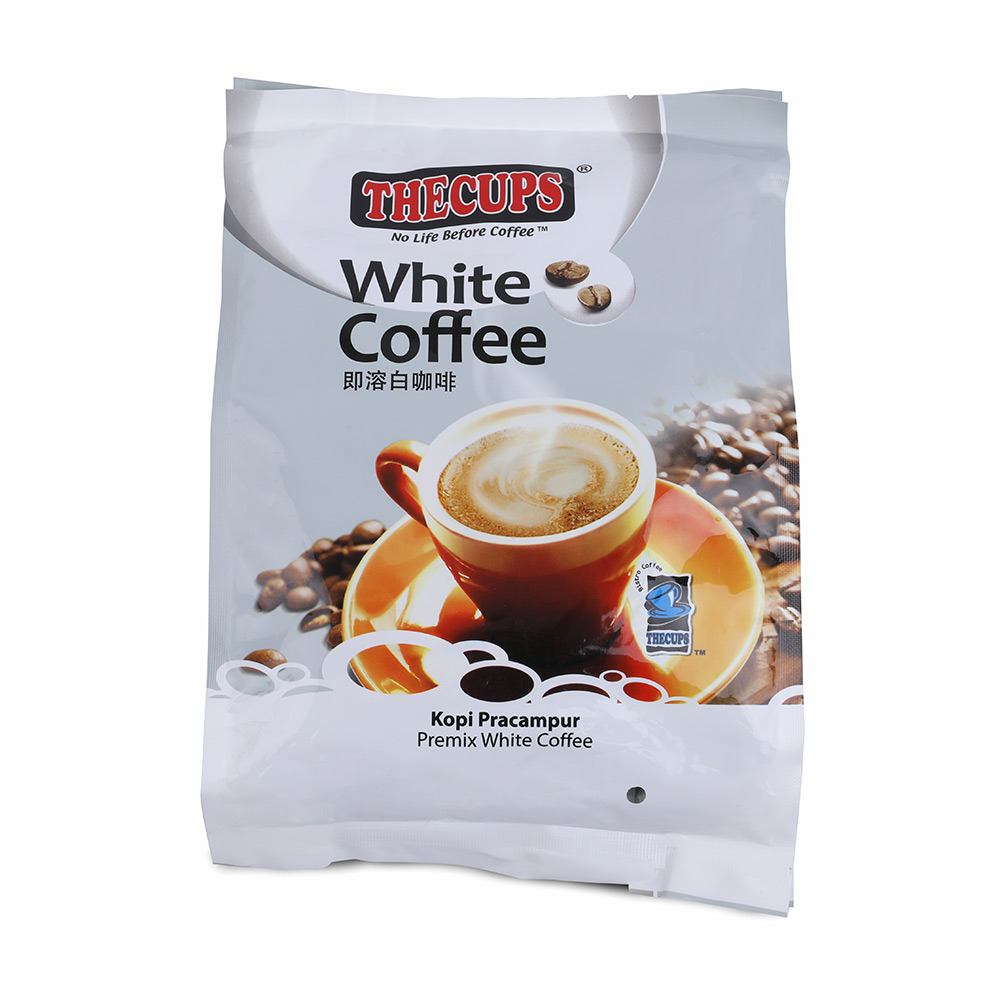 High Barrier Metallized PET Film for Oxygen-Sensitive PackagingA plasma-treated metallized PET film with excellent oxygen and moisture barrier, ideal for biscuits, snacks, and dried fruits. Its glossy appearance enhances shelf presence while providing good lamination strength.View Product → High-barrier metallized CPP film
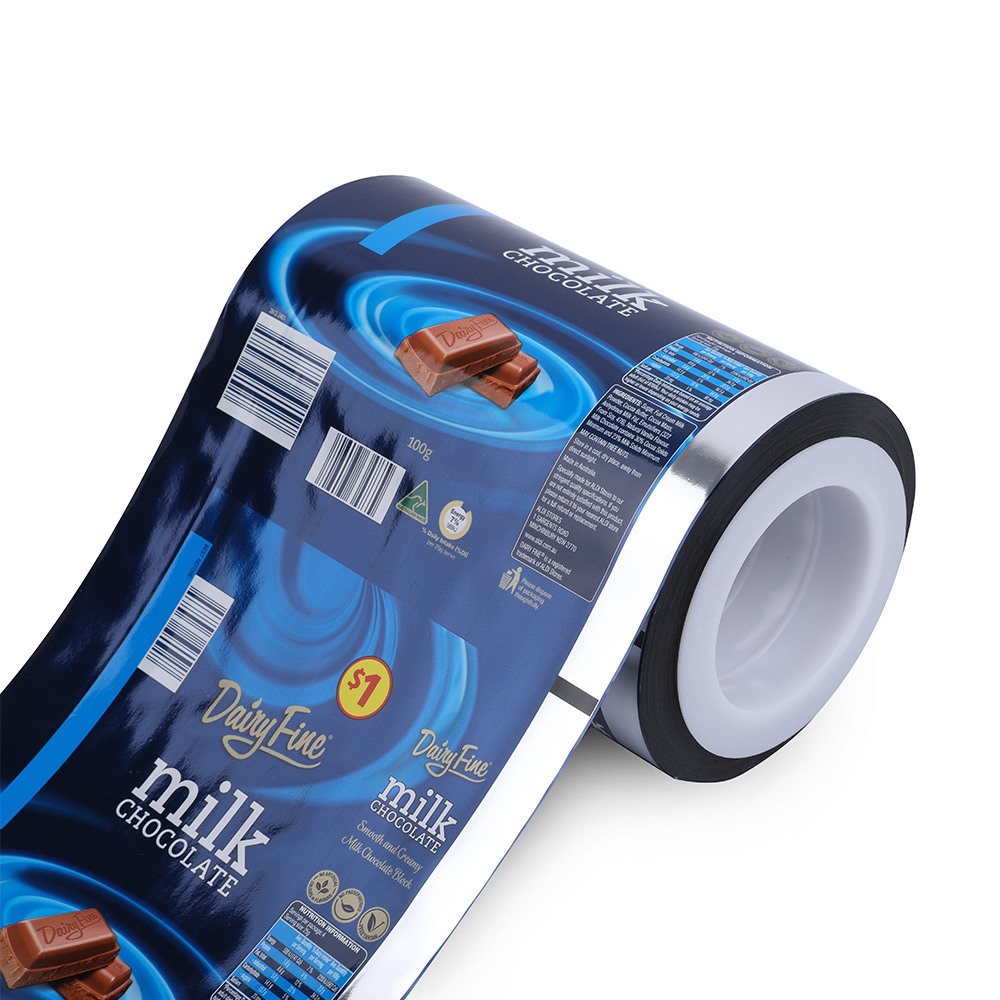 Heat-Sealable Metallized CPP Film with High Barrier PropertiesThis metallized cast polypropylene film combines strong barrier performance with a heat-sealing layer, making it suitable for two-layer food and medicine packaging. Its aluminum adhesion ensures reliable protection.View Product →
These films combine barrier performance with good printability and lamination strength. They are widely used for snacks, dried fruits, coffee, and other oxygen-sensitive products where opacity is acceptable.
Transparent High-Barrier Films
For products where consumers need to see the contents, transparent high-barrier films are the preferred solution. ALOx-coated PET films use aluminum oxide deposited at the nanometer level to create a clear, colorless barrier layer that blocks oxygen without sacrificing visual presentation.
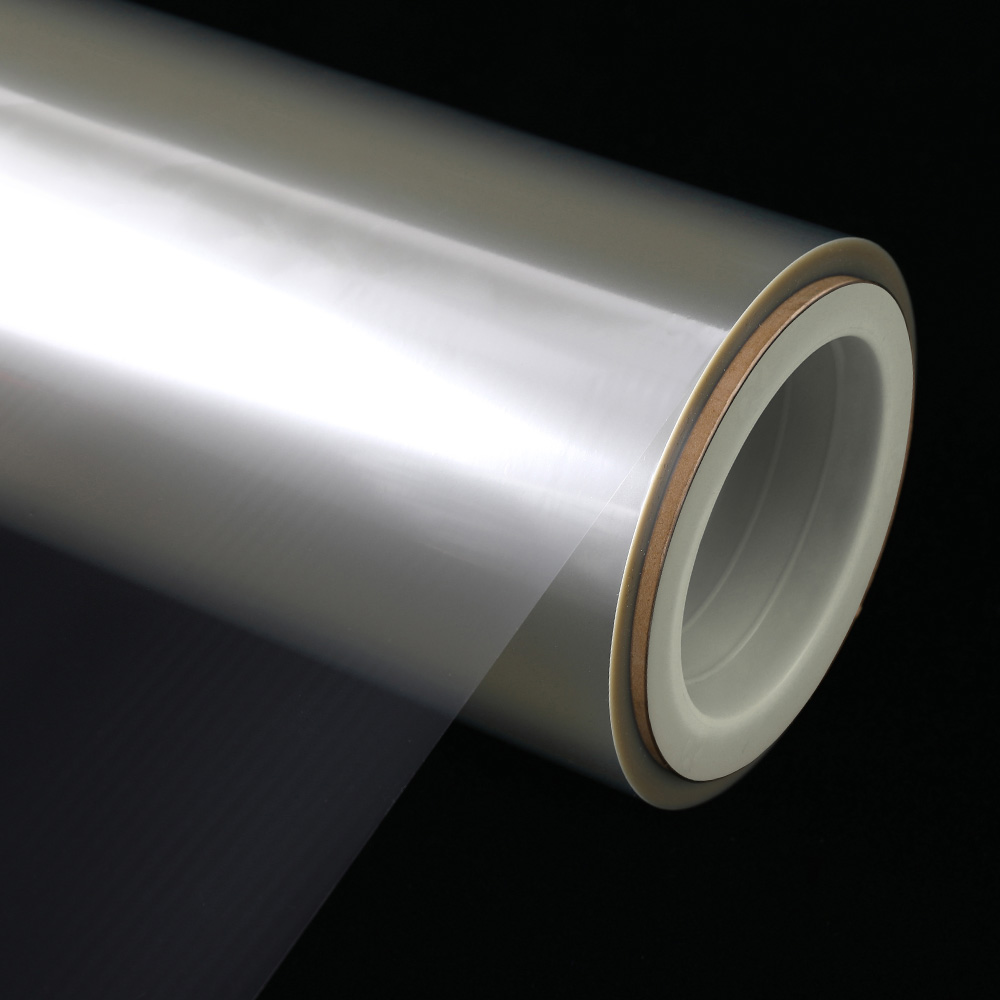
ALOx PET film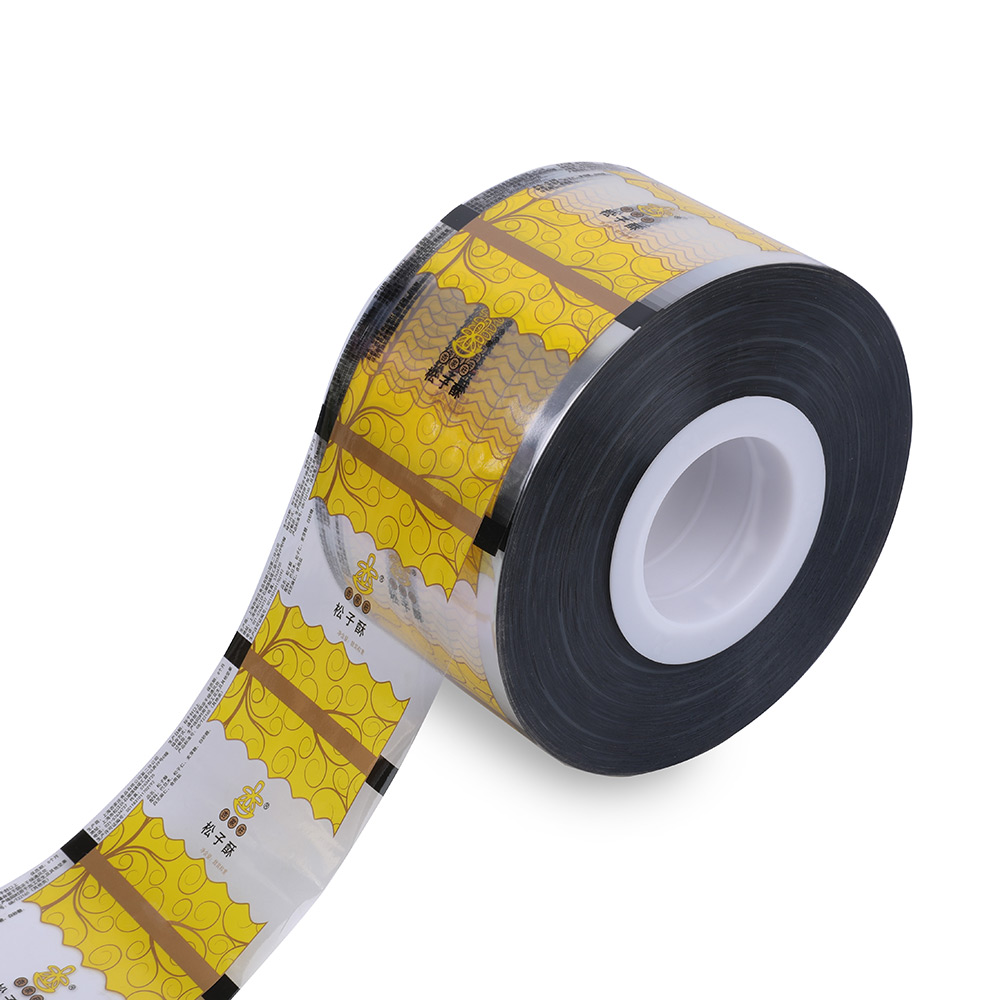 Transparent ALOx-Coated PET Film for Visible PackagingA clear, high-barrier PET film coated with aluminum oxide that blocks oxygen and moisture while maintaining transparency. Suitable for coffee, tea, and nuts where product visibility is key.View Product →
ALOx films deliver OTR values comparable to metallized films while maintaining full transparency. They are especially valuable for coffee, tea, nuts, and other oxygen-sensitive products where brand owners want the package to showcase the product.
Coated Films
PVDC-coated, PVA-coated, and acrylic-coated films provide moderate to high oxygen barrier and additional functional properties such as aroma retention and chemical resistance. PVDC-coated BOPA films, for example, are widely used in retort and boil-in-bag applications where barrier performance must survive heat processing.
How to Choose the Right Oxygen Barrier
Selecting the optimal oxygen barrier material involves evaluating several factors. The most important are:
- Oxygen sensitivity of the product: Coffee, nuts, oils, and processed meats are highly sensitive and require low OTR. Dry goods like sugar and flour are less demanding.
- Target shelf life: Each additional month of shelf life lowers the required OTR. A product needing 12 months of protection requires significantly more barrier than one needing 3 months.
- Transparency requirement: Metallized films are opaque; ALOx films are not. The final consumer experience sometimes depends on being able to see the product.
- Process compatibility: The film must withstand printing, lamination, heat sealing, and in some cases retort conditions without losing barrier performance.
- Cost per square meter: Barrier performance has a direct cost impact. Matching the barrier level to the actual product requirement avoids overspending.
The best oxygen barrier is not always the highest-performing one. It is the one that matches the product's true oxygen sensitivity while remaining compatible with your existing packaging line.
In practice, the first question to answer is whether the package requires transparency. If opacity is acceptable, metallized films deliver the highest barrier-to-cost ratio. If transparency is required, ALOx-coated PET is the natural choice.
For a deeper comparison of how different barrier materials affect actual product shelf life, see how ALOx and metallized films deliver superior barrier performance.
When the product needs to be transparent but the packaging process involves high humidity or demanding temperature conditions, the selection of transparent high-barrier film becomes a critical decision point.
Oxygen Barrier Packaging in Practice: Applications Across Industries
Oxygen barrier packaging is used in a wide range of industries, each with different requirements and performance priorities.
Snacks and Dried Fruits
Metallized films are widely used for chips, nuts, and dried fruits. They provide both oxygen and moisture barrier, keeping products crisp and preventing oil oxidation. The reflective appearance also enhances shelf impact in retail environments.
Coffee and Tea
Coffee beans and tea leaves are extremely oxygen-sensitive. A high barrier film with low OTR is essential for preserving aroma and freshness. Both metallized PET and ALOx-coated PET are common choices, with degassing valves often integrated into the structure.
Cold Meats and Prepared Dishes
Sliced meats, ready-to-eat meals, and sauces require oxygen barrier combined with mechanical strength and often heat resistance. High-barrier structures using metallized films, PVDC-coated films, or ALOx films are used depending on whether transparency is needed.
Pharmaceutical and Medical Packaging
Pharmaceutical packaging requires consistent barrier performance plus regulatory compliance. Transparent high-barrier films are often preferred for blister lidding and strip packaging because they allow visual inspection of tablets and caplets while protecting against moisture and oxygen.
FAQ: Common Questions About Oxygen Barrier Packaging
Q1: What OTR value is considered high barrier for packaging?
As a general industry guideline, films with OTR below 10 cc/m²/day are considered high barrier. For truly oxygen-sensitive products like coffee or pharmaceuticals, OTR below 1 cc/m²/day is typically required.
Q2: Can transparent films match metallized films in oxygen barrier performance?
Yes. ALOx-coated PET films can achieve OTR values in the same range as metallized PET films, typically 0.5-3 cc/m²/day. The advantage of ALOx films is that they remain transparent, allowing consumers to see the product.
Q3: How does film thickness affect oxygen barrier?
Generally, increasing film thickness decreases oxygen transmission. However, the effect is more pronounced for some materials than others. A thicker metallized layer or oxide coating typically provides better barrier than increased base film thickness.

Are you ready to work with us?
Start a project
- Quick Links
- Company Profile
- Company Culture
- Qualification
- FAQ
- Product
- ALOx Films
- VMPET
- VMCPP
- VMBOPP
- Coated Film
- Contact Us
- Tel: +86-13456263964
-
Phone : +86-0573-87783633
Phone : +86-0573-87780583 - E-mail : [email protected]
- Address: 6th Xinhe Road, Xieqiao Town, Haining City, Zhejiang Province, China

